 Products / 02 — Aerospace Tooling
Aerospace tooling, from pattern to production.
A composite part takes its shape, and its errors, from the tool it cures on. Janicki has built that tooling since 1993: masters, layup molds, cure tools, barrel mandrels, cauls, bond jigs, trim-and-drill and assembly fixtures, in composite, Invar, steel and aluminum, on our own 5-axis mills with envelopes to 100 feet.
Signature program
787 fuselage layup mandrels
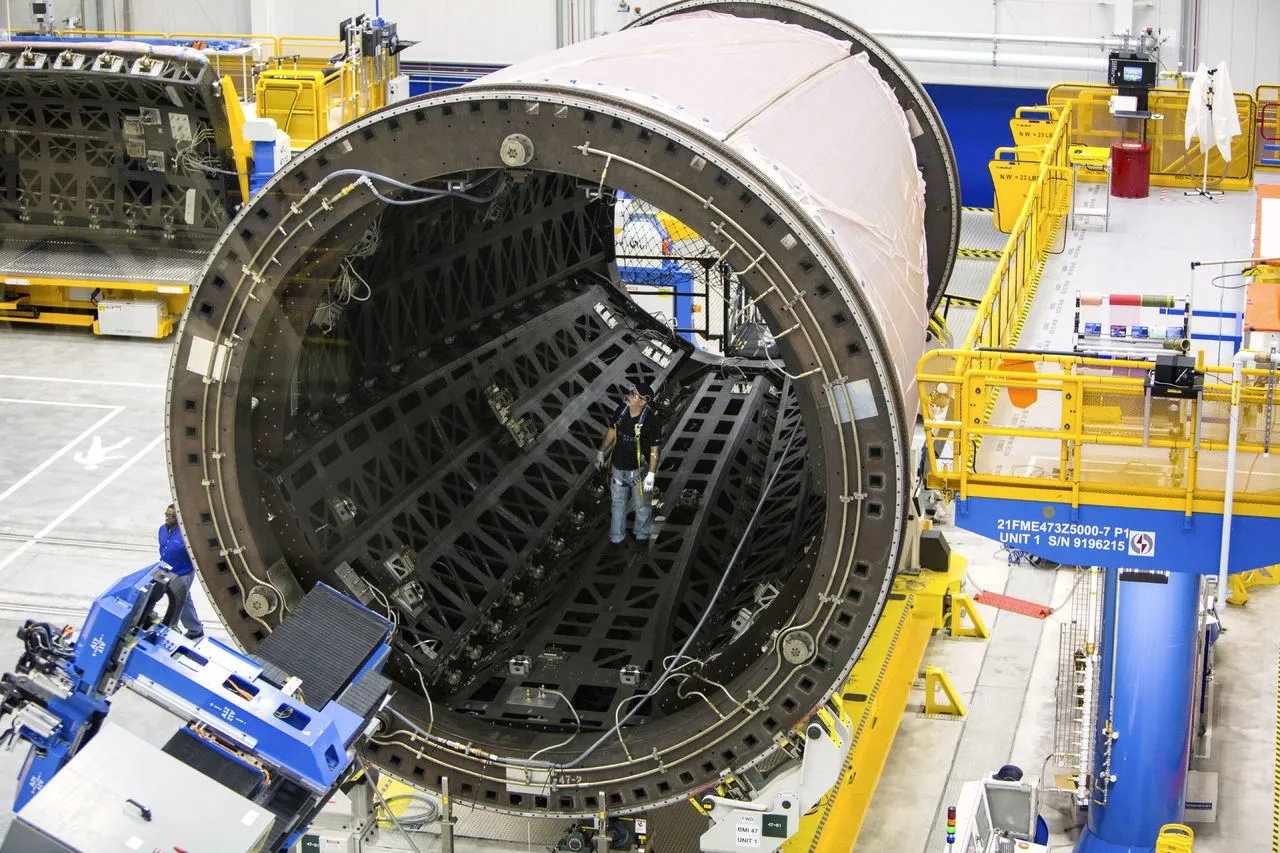
Eight of the mandrels the 787's one-piece composite fuselage barrels are laid up on were built here, in carbon composite rather than metal. A barrel mandrel is the male tool a whole fuselage section is wound and cured around, then extracted from inside the part. Janicki's aft-fuselage mandrels were roughly 20 feet in diameter and 50 feet long, built in composite. Janicki has supported the program since 2006, for Vought and then Boeing — the largest composite tooling in commercial aerospace.
| Item | Detail |
|---|---|
| Program | Boeing 787 aft-fuselage layup mandrels |
| Customer | Vought Aircraft Industries, then Boeing (Boeing South Carolina) |
| Size | ~20 ft diameter × ~50 ft long |
| Material | Carbon composite |
Tooling across the build sequence
Every tool a composite structure needs.
Tooling follows the part through its life: master, mold, trim, drill, bond and assembly fixtures, and the hardware that carries it. Janicki builds all of them, so one set of datums runs from first master to final jig.
Master models and patterns
The form a composite tool is laminated from: putty patterns on wood or steel frames, machined tooling board, foam and MDF, and high-temperature masters that survive the tool's first cure. Machined to ±0.010–0.020 in profile.
Layup molds and cure tools
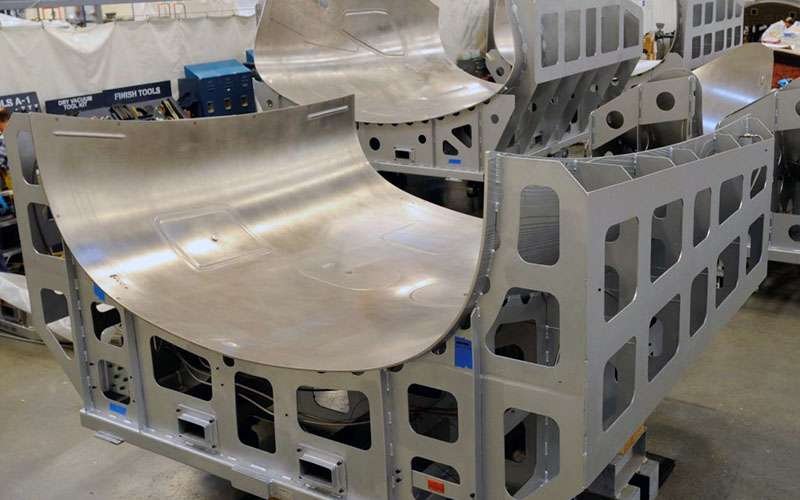
The tool a part is laid on and cured against, OML- or IML-controlled. Composite tools at 250°F and 350°F (cast to ±0.010 in, machined to ±0.005 in, 32 rms) on steel-tube or composite egg-crate substructure; Invar 36, steel and aluminum tools to 100 × 20 × 8 ft; fiber-reinforced tools to 250 ft, spliced. Each ships with a laser-tracker profile report and vacuum-integrity test.
Mandrels
Male tools a part is wrapped around (barrels, spars, ducts, tanks), including breakdown mandrels that disassemble inside a cured one-piece barrel, designed around thermal growth before anything else.
Caul plates and sheets
The bag-side plate that gives a cured part a second controlled surface and uniform thickness, for room-temperature, 250°F and 350°F cure, finished to 8 rms.
Trim and drill fixtures
Vacuum and clamp fixtures that hold a cured part to datum for 5-axis routing and drilling, run at rate in Layton, Utah since 2010.
Bond assembly jigs
Fixtures that locate skins, stringers and ribs through an adhesive cure, oven- and autoclave-cycled, with the same CTE and thermal-survey discipline as a cure tool.
Assembly jigs and fixtures
Tabletop to free-standing jigs that locate details for drilling and fastening, including determinate-assembly designs whose machined locating features need no field setting.
Handling, transport and check fixtures
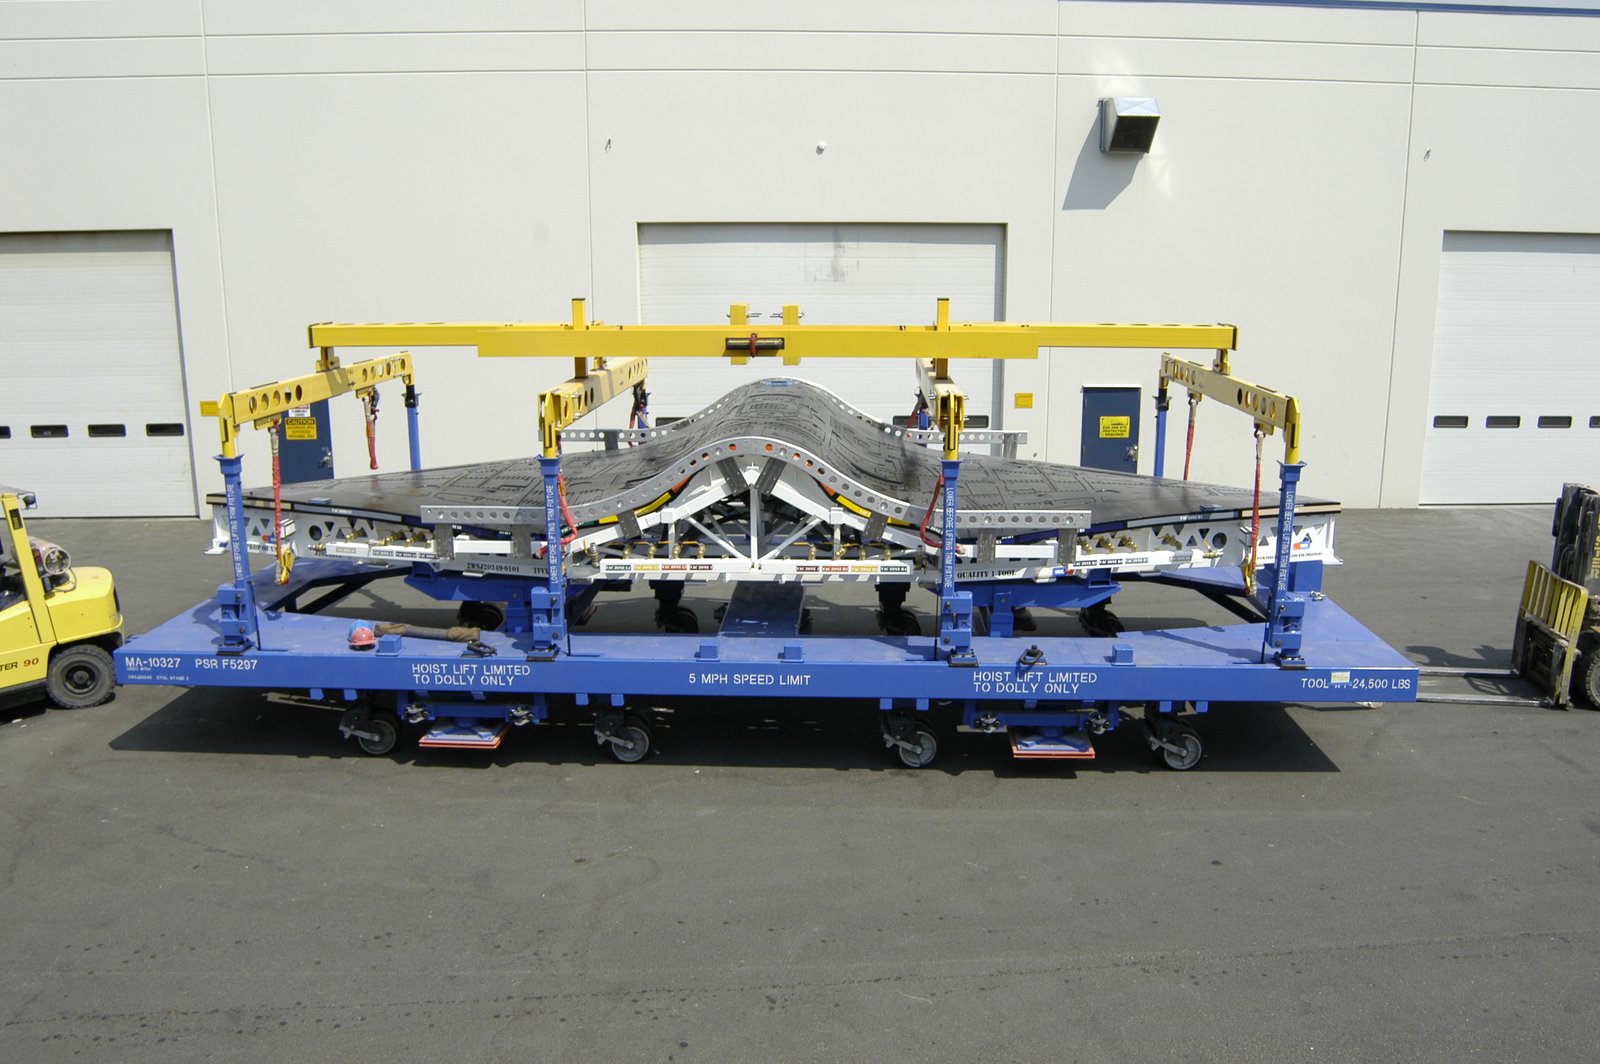
Lift and rotation fixtures, dollies and shipping frames, proof-loaded for what they carry, and check fixtures that verify contour and edge trim.
Materials by cure temperature
Tool material and cure temperature are chosen together.
Carbon/epoxy grows about 1–2 millionths of an inch per inch per °F; aluminum about twelve times as much. The part gels hot and cools on a shrinking tool, so material, cure temperature and surface compensation are chosen together.
| Tier | Materials | Typical use | Tolerance / notes |
|---|---|---|---|
| Patterns · RT–180°F | Proprietary putty on wood or steel frames; tooling board, foam, MDF | Masters, splash patterns, prototype molds | ±0.010–0.020 in · modifiable · 80-grit to machined primer |
| 250°F composite | Carbon or glass/epoxy facesheet, infused or prepreg, on steel-tube or composite egg-crate | Production layup molds for 250°F epoxy parts | Cast ±0.010 in · machined ±0.005 in · laser-tracked and vacuum-verified |
| 350°F composite | Carbon/BMI, benzoxazine or epoxy tooling laminates; low-temperature-demold BMI prepreg co-developed with Kaneka | Production molds and mandrels for 350°F aerospace epoxies; one-fifth the density of Invar | Cast ±0.010 in · machined ±0.005 in · 32 rms · 500+ cycle class |
| Invar 36 | Welded plate facesheet on egg-crate; 1,500+ qualified weld procedures; annealed in-house (72′ × 24′ × 11′ furnace, 1,750°F) | Highest-life production tools, CTE ~1.5 ppm/°F to cure temperature | To 100 × 20 × 8 ft · thousands of cycles |
| Steel · aluminum | Machined or welded | Small and scalable parts, cauls, trim and assembly fixtures, press tools | Fast and low cost; CTE managed by scaling the tool |
| Fiber-reinforced plastic | Glass/polyester and vinyl-ester with core | Very large low-temperature molds — marine and full-scale masters | To 250 ft long |
Tolerances are profile-to-CAD by laser tracker; program specifications govern.
Program experience
Tooling that has been through a program.
A selection from three decades of published work.
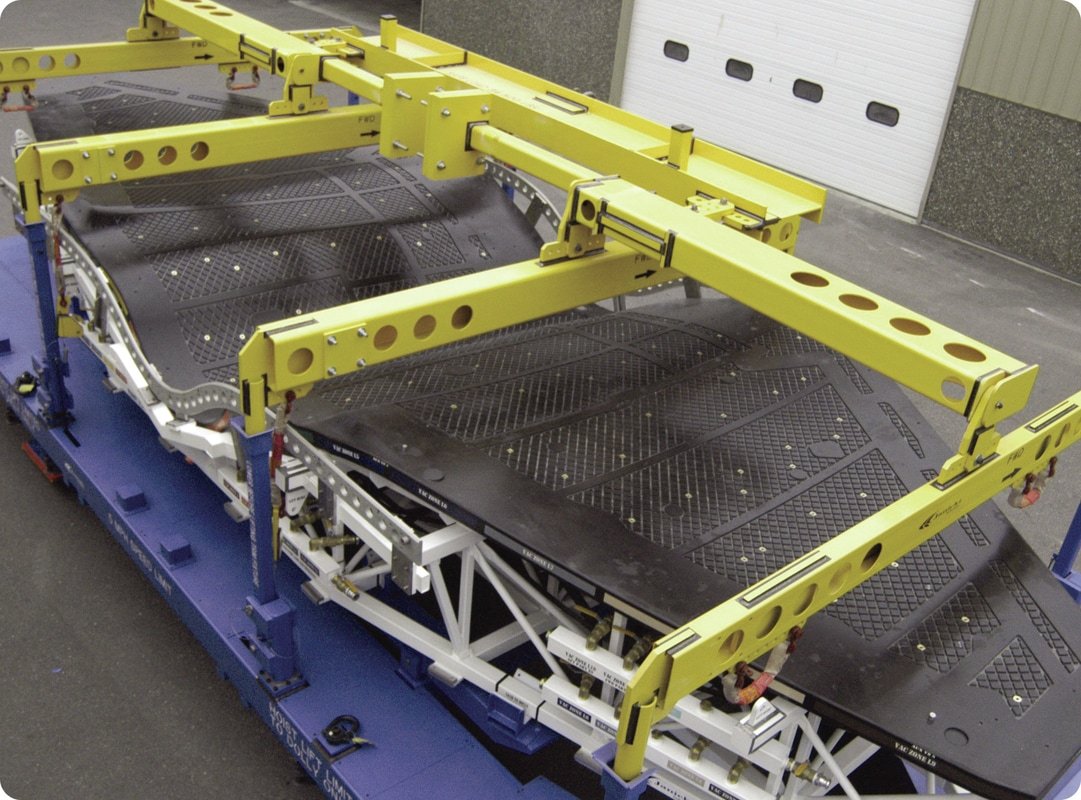
NASA — SLS payload fairing
One-sixth-arc layup tool: 561 sq ft of carbon/epoxy facesheet, infused and cured out of autoclave with a BMI top coat, ±0.020 in profile over 28 ft.
Bombardier — CSeries wing
Two-piece stringer-mold inserts for the resin-infused composite wing: the soft tooling inside an Invar outer-mold-line tool.
Stratolaunch
Molds for the widest wingspan ever flown, then roughly 40% of the aircraft's structure by weight, tooling and parts from the same floor.
Sikorsky — S-97 Raider
350°F epoxy tooling delivered in 60 days for the prototype program.
Recognition
Boeing Supplier of the Year 2023; Northrop Grumman Supplier Excellence Awards 2024 and 2025; JEC Innovation Award 2017; CompositesWorld Top Shop 2020.
Start a tool
Bring us the tool drawing.
Send us the geometry, cure temperature and cycle count; we will propose material, substructure and schedule.